Introduction
Quality Checks During Granulation
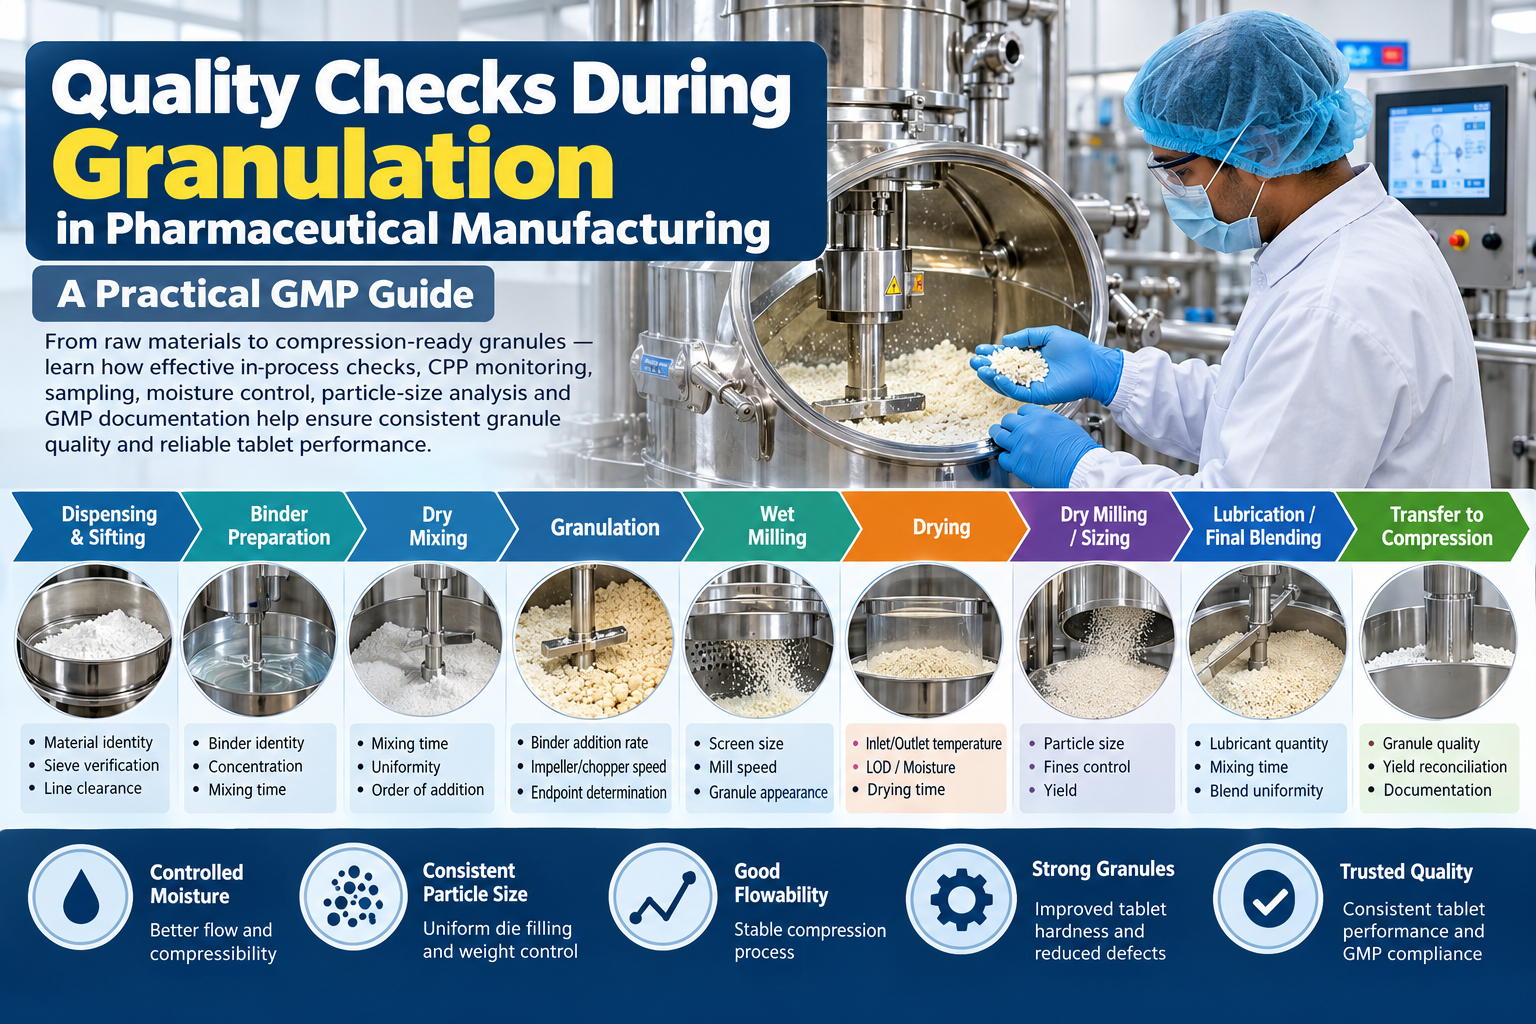
From raw materials to compression-ready granules — learn how effective in-process checks, CPP monitoring, sampling, moisture control, particle-size analysis and GMP documentation help ensure consistent granule quality and reliable tablet performance.
A granulation batch can look perfectly normal from the outside and still create problems later at compression.
This is something manufacturing professionals learn quickly on the shop floor. A small difference in binder preparation, wet-mass consistency, drying, milling or lubrication can eventually appear as poor flow, weight variation, sticking, picking, capping, lamination, hardness variation or dissolution problems during compression and finished-product testing.
Granulation is therefore not simply a step used to convert powder into granules. It is a controlled manufacturing operation in which several material and process variables have to remain within the established process strategy.
During tablet manufacturing, granulation can influence:
- Granule size distribution
- Flowability
- Compressibility
- Bulk and tapped density
- Moisture content
- Blend uniformity
- Die filling
- Tablet weight variation
- Tablet hardness
- Friability
- Disintegration
- Dissolution
- Content uniformity
The practical objective is not to make the granules “look good.” The objective is to consistently produce granules with the characteristics required for the next manufacturing stage.
GMP expects manufacturing processes to be appropriately controlled, documented and capable of producing material meeting established quality requirements. FDA’s CGMP framework specifically addresses written production procedures, yield calculations, in-process sampling/testing and production record review, while FDA’s process-validation guidance emphasizes a lifecycle approach to process understanding and control.
That is why quality checks during granulation should be considered process controls, not merely laboratory tests.
Important: The actual acceptance criteria, sampling frequency, operating ranges and testing responsibilities must always come from the approved BMR/BPR/MFR, product specification, validated process, SOPs, protocols and site quality system. The examples below explain the principles and typical controls; they are not universal acceptance limits.
1. What is Granulation?
Granulation is a particle-size enlargement process in which smaller powder particles are converted into larger, more cohesive granules.
In tablet manufacturing, granulation is generally performed to improve characteristics such as:
- Flowability
- Compressibility
- Content uniformity
- Handling characteristics
- Dust control
- Die-filling behavior
There are two broad approaches:
Wet Granulation
In wet granulation, a binder solution or granulating liquid is introduced into a powder blend under controlled mixing conditions. The resulting wet mass is then milled, dried and sized.
A typical sequence is:
Dispensing → Sifting → Binder Preparation → Dry Mixing → Wet Granulation → Wet Milling → Drying → Dry Milling/Sizing → Lubrication/Final Blending → Transfer
Dry Granulation
Dry granulation does not use a conventional liquid binder solution. Powder is compacted using techniques such as slugging or roller compaction and subsequently sized.
This article focuses mainly on wet granulation used for OSD tablet manufacturing.
Why Granulation Matters to Compression
The compression machine does not compensate for every problem created upstream.
For example:
Poor drying → incorrect moisture → altered granule properties → poor flow/compressibility → compression variation
Similarly:
Excessive binder → stronger/dense granules → altered disintegration/dissolution behaviour
or:
Aggressive milling → excessive fines → poor flow → inconsistent die filling → tablet weight variation
The quality of the tablet is therefore strongly influenced by the quality of the granules entering compression.
2. Quality Control Points Across the Granulation Process
A practical quality-control approach follows the complete process rather than checking only the finished granules.
| Stage | Major Quality Focus |
|---|---|
| Dispensing | Identity, status, quantity, material condition |
| Sifting | Correct screen/mesh, integrity, cleanliness |
| Binder preparation | Concentration, quantity, mixing, appearance, holding |
| Dry mixing | Sequence, time, speed, load, uniformity where applicable |
| Wet granulation | Binder addition, speed, time, endpoint, torque/current |
| Wet milling | Screen, speed, feed rate, granule condition |
| Drying | Temperature, airflow, time, product temperature, moisture |
| Dry milling | Particle-size distribution, fines, oversized granules |
| Lubrication | Lubricant quantity, mixing time/speed, blend quality |
| Transfer | Identification, yield, container integrity, status and protection |
At each stage, the key question should be:
“What characteristic am I controlling now, and what downstream problem could occur if I lose control?”
3. Pre-Granulation Quality Checks
3.1 Dispensing
Before starting manufacturing, the first quality decision is whether the correct materials are being introduced into the batch.
Typical checks include:
Material identity
Verify:
- Material name/code
- Batch/lot number
- Status label
- Approved/released status
- Expiry or retest status
- Container integrity
Material identification should be independently verified according to the site’s approved procedure.
Quantity
Check the dispensed quantity against the approved manufacturing instruction.
The weighing system should be suitable, within calibration and appropriate for the intended weighing operation.
Equipment and area checks
Before dispensing and processing:
- Area status should be acceptable.
- Line clearance should be completed.
- Equipment should have the correct clean/status identification.
- Previous product/material remnants should not be present.
- Required documents should be available.
- Applicable environmental conditions should be within established requirements.
FDA’s CGMP framework includes controls for materials, equipment, written procedures and production/process controls.
If something is wrong
Do not simply correct the entry and continue.
Examples:
- Wrong material identified
- Quantity discrepancy
- Expired/retest-due material
- Balance calibration issue
- Incorrect equipment status
These should be handled according to the applicable SOP and quality-system procedure, including escalation or deviation assessment where required.
4. Sifting Checks
Sifting appears simple, but incorrect screening can influence the entire downstream process.
Check:
- Correct sieve/screen identification
- Correct mesh size
- Sieve integrity
- Cleanliness
- Physical condition
- Correct assembly
- Sifting sequence
- Material identity
- Foreign-material prevention
The sieve should be inspected before use and, where required by procedure, after completion.
Why sieve selection matters
A finer or coarser screen than specified can change the particle-size distribution entering granulation.
That can influence:
- Mixing
- Binder distribution
- Granule formation
- Granulation endpoint
- Drying behaviour
- Final particle-size distribution
- Compression performance
A useful shop-floor principle is:
Do not treat the sieve as just a piece of equipment. Treat it as a process input.
5. Binder Preparation Checks
Binder preparation is one of the most underestimated quality controls in wet granulation.
The binder solution can influence granule formation, strength and subsequent drying.
Typical checks include:
- Correct binder identity
- Correct quantity
- Correct solvent/vehicle
- Concentration
- Mixing time
- Mixing speed
- Temperature where applicable
- Appearance/clarity where specified
- Final volume where applicable
- Holding time
- Storage conditions
Why Binder Concentration Matters
If the binder concentration or preparation is incorrect, the resulting wet mass may behave differently even when the granulator settings appear normal.
Potential consequences include:
Higher-than-intended binder effect
→ stronger or denser granules
→ altered drying behaviour
→ possible impact on milling
→ possible compression and dissolution effects
Lower-than-intended binder effect
→ weak granules
→ increased fines
→ poor flow
→ possible compression problems
Therefore, binder preparation should be controlled as carefully as the granulation itself.
6. Dry Mixing Checks
Before binder addition, the powders generally undergo a controlled dry-mixing operation.
Check:
- Correct material addition sequence
- Equipment status
- Equipment load
- Mixing time
- Mixing speed
- Product temperature where relevant
- Sampling requirements
- Blend uniformity where applicable
The purpose is to establish appropriate distribution of the formulation components before liquid addition.
Poor dry mixing can create problems that are difficult to correct later.
For example:
Inadequate mixing → non-uniform distribution → granulation locks the distribution into agglomerates → downstream uniformity problem
This is particularly important when the formulation contains a low-dose active ingredient.
7. Wet Granulation Process Checks
This is the central control point of the process.
During wet granulation, operators, production supervisors and IPQA personnel may monitor several process parameters depending on the equipment and validated process.
Important Critical Process Parameters
Typical parameters may include:
- Binder quantity
- Binder addition rate
- Impeller speed
- Chopper speed
- Granulation time
- Granulator load
- Product temperature
- Torque/current/power trend
- End-point indicators
Not every parameter is necessarily a CPP for every product.
The CPP designation should come from the product/process knowledge, risk assessment, development work and validated control strategy.
ICH Q8/Q9/Q10 provides a science- and risk-based framework for pharmaceutical development, quality risk management and the pharmaceutical quality system.
Binder Addition Rate
Binder addition is not simply a matter of adding the specified quantity.
The rate of addition can influence how evenly the liquid is distributed.
Too rapid an addition can promote localized overwetting.
Too slow or poorly distributed addition can produce inconsistent granulation.
Therefore, the approved process should define the required approach.
Impeller Speed
Impeller speed influences mixing intensity and wet-mass formation.
Changes can affect:
- Binder distribution
- Granule growth
- Shear
- Granule density
- Endpoint behaviour
The effect is formulation- and equipment-dependent.
Chopper Speed
The chopper influences wet-mass breakdown and granule-size development.
Excessive or inadequate chopping can alter the resulting granule structure.
Again, the correct condition is the validated condition for the particular product and equipment.
8. How is the Granulation Endpoint Determined?
The granulation endpoint is the point at which the wet mass has reached the required condition for subsequent processing.
There is no universal endpoint value that can be applied to every product.
Depending on the process, endpoint determination may use:
- Torque trend
- Motor current/power trend
- Granule appearance
- Wet-mass consistency
- Approved hand-squeeze test
- Product temperature
- Process trend
- Time-based criteria
- Validated equipment-specific endpoint criteria
Torque or Current Trend
Modern high-shear granulators may provide a useful process signal through torque, power or motor-current behaviour.
As granulation develops, the mechanical resistance experienced by the impeller can change.
A validated relationship between the process signal and granule condition can therefore be useful.
However:
An operator should not simply stop the granulation because the torque “looks high.”
The interpretation must be based on the approved process and established endpoint criteria.
Granule Appearance
Appearance can provide useful supporting information.
An experienced operator may observe:
- Wet mass consistency
- Formation of granules
- Excessive lumps
- Excessive free powder
- Excessive wetness
But visual assessment should support—not replace—the approved validated endpoint approach.
Hand Squeeze Test
Some processes use a controlled hand-squeeze or similar manual test.
If used, the method must be defined and appropriately controlled. It should not become an informal operator-dependent test where different operators use different interpretations.
9. In-Process Quality Checks During Granulation
The following represents a practical framework. The exact frequency and responsibility depend on the approved batch record and site SOP.
| Quality Check | Purpose | Typical Method | Typical Timing/Frequency | Impact |
|---|---|---|---|---|
| Appearance | Detect abnormal wet-mass/granule condition | Visual examination | As defined | Early detection of abnormal granulation |
| Wet-mass consistency | Assess granulation development | Approved process method | During/at endpoint | Granule quality |
| Moisture/LOD | Control residual moisture | Approved analytical method | After drying / defined IPC point | Flow, compression, stability |
| Particle size | Assess granule distribution | Sieve analysis or validated method | Defined stage | Flow and compression |
| Bulk density | Assess packing characteristics | Approved method | Defined IPC | Die filling |
| Tapped density | Assess packing behaviour | Approved method | Defined IPC | Flow/compressibility |
| Flow properties | Assess handling/die filling | Approved method | Where applicable | Weight variation |
| Granule yield | Reconcile material | Calculation | Batch stage | Material accountability |
| Product temperature | Monitor thermal/process condition | Calibrated instrument | Where applicable | Product/process control |
| Sieve analysis | Control size distribution | Sieve method | Defined stage | Compression behaviour |
The point of IPC testing is not to generate numbers for the batch record. Each test should have a defined connection to product or process quality.
FDA specifically identifies sampling and testing of in-process materials as part of CGMP production/process controls.
10. Wet Milling Checks
Wet milling converts the wet mass into particles suitable for drying.
Check:
- Correct screen size
- Screen integrity
- Correct mill configuration
- Mill speed
- Feed rate
- Product temperature where applicable
- Granule appearance
- Equipment cleanliness
- Yield/reconciliation
Excessive Fines
Possible causes can include:
- Excessive milling intensity
- Incorrect screen
- High mill speed
- Low feed rate
- Weak granules
- Over-dried or otherwise abnormal upstream material
Oversized Granules
Possible causes may include:
- Incorrect screen
- Insufficient milling
- Wet-mass condition
- Inadequate granulation
- Equipment/feed issues
The investigation should consider the entire process rather than immediately changing the milling speed.
11. Drying Process Quality Checks
Drying is another stage where the process can appear normal while the final granule quality moves outside the desired condition.
Typical process checks include:
- Inlet temperature
- Outlet temperature
- Product temperature
- Airflow
- Drying time
- Equipment load
- Sampling
- LOD/moisture
- Uniformity of drying
The validated process should establish the relationship between these process parameters and the required final granule condition.
Under-Drying
Potential consequences include:
- Excessive residual moisture
- Sticking during compression
- Poor flow
- Altered tablet properties
- Stability concerns
- Microbiological concerns where relevant
Over-Drying
Potential consequences can include:
- Brittle granules
- Excessive fines
- Reduced compressibility
- Capping or lamination
- Changes in dissolution behaviour for some formulations
These are not automatic outcomes for every formulation. The actual impact must be understood from product/process development and investigation data.
LOD Is More Than a Number
LOD or moisture testing is often treated as a simple pass/fail test.
From a manufacturing perspective, it is better viewed as one indicator of the physical state of the granules.
The relationship can be thought of as:
Drying conditions → moisture → granule structure → flow/compression → tablet performance
That is why a failed LOD result should trigger process investigation rather than simply “drying again” without assessment.
12. Dry Milling / Sizing
After drying, granules are normally sized to establish the required particle-size distribution.
Check:
- Correct screen
- Screen integrity
- Mill speed
- Feed rate
- Particle-size distribution
- Fines
- Oversized granules
- Equipment condition
- Yield
Why Particle Size Matters
Particle-size distribution can influence:
Flow → hopper movement → die filling → tablet weight
It can also influence:
Particle packing → compression behaviour → hardness/friability
Therefore, particle-size analysis is an important bridge between granulation and compression.
A batch can have acceptable average moisture and still compress poorly if the particle-size distribution is significantly different from the established process condition.
13. Lubrication / Final Blending
Lubrication is sometimes considered the final simple mixing step.
It should not be.
The final blending operation can have a significant impact on tablet performance.
Check:
- Lubricant identity
- Lubricant quantity
- Order of addition
- Mixing time
- Mixing speed
- Blend uniformity where applicable
- Bulk density
- Flow
- Granule appearance
The Risk of Over-Lubrication
Many tablet formulations use lubricants such as magnesium stearate.
Excessive lubrication or excessive mixing can change particle surfaces and affect interparticle bonding.
Potential consequences can include:
- Reduced tablet hardness
- Increased disintegration time
- Dissolution impact
- Changes in tablet bonding
- Other compression-related effects
The correct lubrication time and mixing intensity must therefore be based on formulation and validated process knowledge.
14. Sampling Plan During Granulation
Good testing depends on good sampling.
A technically perfect analytical method cannot compensate for an unrepresentative sample.
Sampling Locations
The sampling plan should define appropriate locations based on the process and equipment.
Depending on the stage, sampling may consider:
- Different container locations
- Different portions of a batch
- Beginning/middle/end where justified
- Multiple points in a blender
- Appropriate locations after milling/drying
Sampling should be scientifically justified rather than based solely on convenience.
Sampling Tools
Tools should be:
- Appropriate for the material
- Clean
- Identified where required
- Suitable for the intended sampling operation
- Used according to the approved sampling procedure
Representative Sampling
Suppose a batch contains a mixture of coarse and fine granules.
Taking one scoop from the top of a container may not represent the entire batch.
Similarly, one sample from one location in a blender may not demonstrate uniformity throughout the blend.
The sampling plan should therefore consider the risk of segregation and process variability.
Sample Identification
Samples should be traceable to:
- Product
- Batch number
- Stage
- Sample location where applicable
- Date/time
- Sampler
- Test requirement
Sample handling and storage should prevent contamination, mix-up or changes in the sample condition.
15. Critical Quality Attributes in Granulation
A CQA is a physical, chemical, biological or microbiological characteristic that should be controlled within an appropriate range, limit or distribution to ensure the desired product quality.
For granulation, relevant CQAs may include:
| CQA | Why It Matters | Potential Impact |
|---|---|---|
| Moisture/LOD | Controls residual moisture | Flow, compression, stability |
| Particle-size distribution | Controls granule population | Flow and die filling |
| Bulk density | Indicates packing characteristics | Compression and weight |
| Tapped density | Indicates packing response | Flow/compressibility |
| Flowability | Supports consistent feeding | Weight variation |
| Granule strength | Determines resistance to handling | Fines generation |
| Fines | Excessive fines can alter flow | Compression problems |
| Yield | Demonstrates material recovery | Reconciliation/process control |
| Blend uniformity | Confirms appropriate distribution | Content uniformity |
Not every listed attribute will be a formal CQA for every product. The classification depends on product knowledge and the established control strategy.
16. CPP vs CQA in Granulation
One of the most common interview questions is:
What is the difference between CPP and CQA?
Critical Process Parameter — CPP
A CPP is a process parameter whose variability can have an impact on a critical quality attribute and therefore needs to be monitored or controlled to ensure the process produces the desired quality.
Examples may include:
- Impeller speed
- Chopper speed
- Binder addition rate
- Binder quantity
- Granulation time
- Drying temperature
- Drying time
- Milling parameters
Critical Quality Attribute — CQA
A CQA is a physical, chemical, biological or microbiological characteristic that should be controlled to ensure product quality.
Examples may include:
- Moisture
- Particle-size distribution
- Density
- Flow
- Granule characteristics
- Blend uniformity where applicable
Simple Relationship
CPP → Granulation Behaviour → CQA → Compression Performance → Tablet Quality
For example:
Binder addition rate
↓
Wet-mass formation
↓
Granule size/strength
↓
Flow + compressibility
↓
Tablet weight + hardness + dissolution
This CPP-CQA relationship is central to a science- and risk-based manufacturing approach. ICH Q8(R2), Q9(R1) and Q10 collectively support pharmaceutical development, risk management and a pharmaceutical quality system approach.
17. Common Granulation Problems and Troubleshooting
The most important troubleshooting principle is:
Do not treat the symptom before understanding the cause.
| Observation | Possible Causes | Investigation | Corrective Approach |
|---|---|---|---|
| Excessive fines | Weak granules, aggressive milling, inadequate binder effect, drying condition | Review binder, endpoint, drying, milling and PSD trends | Address verified root cause |
| Large granules | Excessive wetting, inadequate milling, process condition | Review binder addition, endpoint and screen | Correct process based on investigation |
| Over-wet mass | Excessive liquid, rapid addition, endpoint issue | Check binder quantity/rate and process trend | Follow approved corrective procedure |
| Under-granulation | Insufficient binder effect or mixing | Review formulation, binder preparation and endpoint | Investigate before adjustment |
| Poor flow | Excessive fines, broad PSD, density variation, moisture issue | Review PSD, moisture and density | Correct identified source |
| High moisture | Inadequate drying | Review temperature, airflow, load, drying time | Follow validated drying procedure |
| Low moisture | Excessive drying | Review drying trend and product temperature | Investigate process condition |
| Poor yield | Material loss, transfer loss, milling loss, abnormal fines | Reconcile each process stage | Identify actual loss point |
| Sticking during compression | Moisture, formulation, lubrication, granule condition | Review LOD, granule characteristics and compression data | Investigate upstream/downstream factors |
| Capping | Granule moisture/PSD, air entrapment, compression conditions | Review granulation and compression trends | Determine contributing factors |
| Lamination | Granule properties, compression parameters, lubrication | Review PSD, moisture, lubrication and compression | Root-cause investigation |
| Weight variation | Poor flow, PSD variation, segregation | Review granules and compression feed | Correct flow/segregation cause |
| Dissolution failure | Granule density, binder/lubrication, PSD, formulation/process variation | Compare batch trends with historical/process data | Full product/process impact assessment |
A Better Troubleshooting Sequence
When a problem occurs, ask:
- What exactly changed?
- When did the change first occur?
- Was any CPP outside its approved range?
- Were raw materials within requirements?
- Was equipment functioning correctly?
- Was the endpoint determined correctly?
- Did moisture change?
- Did particle-size distribution change?
- Was the sampling representative?
- Is there a historical trend?
- Could the problem have originated upstream?
- Could it be related to downstream processing?
This approach is much stronger than simply changing one machine parameter.
18. Deviation Handling During Granulation
Examples of situations requiring assessment may include:
- CPP outside the approved range
- LOD failure
- Particle size outside specification
- Unexpectedly low yield
- Equipment malfunction
- Incorrect binder quantity
- Drying time beyond the validated/approved condition
- Incorrect screen used
- Process interruption
- Documentation discrepancy
The response should follow the site’s deviation and quality-system procedures.
A practical sequence is:
Detection
↓
Immediate containment/action
↓
Documentation
↓
Product/process impact assessment
↓
Investigation
↓
Root-cause analysis
↓
CAPA where justified
↓
Effectiveness verification
Example: LOD Failure
Suppose dried granules fail the approved moisture requirement.
The response should not automatically be:
“Put the granules back into the dryer.”
First establish:
- What was the actual result?
- Was the sample representative?
- Was the analytical method/system suitable?
- Were drying parameters within approved conditions?
- Was the equipment functioning properly?
- Was the batch load correct?
- Was airflow adequate?
- Was there an abnormal process interruption?
- What is the potential product impact?
- Has similar behaviour occurred in previous batches?
Any reprocessing/re-drying decision should be governed by approved procedures and appropriate quality assessment.
FDA’s CGMP framework specifically addresses written procedures and deviations, in-process testing and investigation/review of production records.
19. GMP Documentation Requirements
Granulation generates a large amount of GMP documentation.
Typical records include:
- BMR/BPR/MFR
- Dispensing records
- Equipment logbooks
- Cleaning records
- Line-clearance records
- Sieve records
- Mill records
- Binder-preparation records
- IPC records
- Sampling records
- Laboratory results
- Calibration records/status
- Preventive-maintenance status
- Environmental monitoring/conditions where applicable
- Yield reconciliation
- Deviation records
- Equipment usage records
- Transfer records
The principle is straightforward:
If an activity was performed but was not properly documented, demonstrating that it was performed correctly becomes difficult.
ALCOA+ in Granulation
Granulation records should support data that are:
- Attributable
- Legible
- Contemporaneous
- Original
- Accurate
And should also meet the broader ALCOA+ expectations, including:
- Complete
- Consistent
- Enduring
- Available
For example, an operator should not reconstruct process information from memory several hours later simply because the entry was missed.
EU GMP Volume 4 includes dedicated chapters for production, documentation and quality control, reinforcing the role of controlled production and documentation systems.
20. Role of Production, IPQA and QC
Exact responsibilities vary between organizations and SOPs, but a practical division is as follows.
Production
Production generally performs and/or controls:
- Approved process execution
- Equipment operation
- CPP monitoring
- Material sequence
- Binder addition
- Granulation operation
- Drying/milling operations
- Process observations
- In-process checks assigned to Production
- Documentation
- Immediate reporting of abnormalities
The operator is often the first person to recognize that something has changed.
That makes operator observation an important process-control element.
IPQA
IPQA may be responsible for:
- Line clearance verification
- GMP compliance
- In-process verification
- Process observation
- Documentation review
- Sampling oversight where applicable
- Verification of critical steps
- Escalation of abnormalities
- Deviation initiation/escalation as defined by procedure
IPQA should not merely “stand and watch.”
A strong IPQA professional understands why a process parameter matters and what downstream risk it represents.
QC
QC may perform approved laboratory testing such as:
- Moisture/LOD
- Particle-size analysis
- Bulk density
- Tapped density
- Flow-related tests
- Blend testing
- Other approved analytical or physical tests
The specific allocation between Production, IPQA and QC should always follow site procedures.
21. Practical Granulation Checklist
Before Granulation
☐ Line clearance completed
☐ Equipment cleanliness verified
☐ Equipment status verified
☐ Correct materials verified
☐ Material status verified
☐ Dispensed quantities verified
☐ Sieve verified
☐ Sieve integrity checked
☐ Binder verified
☐ Balance/equipment calibration status checked
☐ BMR/BPR available and current
☐ Applicable environmental conditions checked
During Granulation
☐ Correct material sequence
☐ Correct binder quantity
☐ Binder addition rate controlled
☐ Impeller speed verified
☐ Chopper speed verified
☐ Granulation time monitored
☐ Endpoint monitored using approved method
☐ Product condition observed
☐ Abnormal noise/vibration/operation reported
☐ Required IPC samples collected
☐ Observations documented contemporaneously
After Granulation
☐ Wet milling completed as approved
☐ Drying parameters reviewed
☐ LOD/moisture checked
☐ Dry milling completed
☐ Particle size checked
☐ Granule appearance checked
☐ Yield reconciled
☐ Equipment status updated
☐ Samples identified correctly
☐ Documentation completed and reviewed
☐ Deviations documented where applicable
☐ Material transferred under appropriate status
22. Practical Interview Questions and Answers
1. What are the critical parameters during wet granulation?
Typical parameters can include binder quantity and addition rate, impeller speed, chopper speed, granulation time, load and endpoint criteria. The actual CPPs are product- and process-specific.
2. How do you determine granulation endpoint?
Use the approved and validated endpoint method. Depending on the process, this may involve torque/current trend, wet-mass characteristics, granule appearance, time or other established indicators.
3. What happens if too much binder is added?
It can produce excessively wet or stronger/dense granules and may alter drying, milling, compression and dissolution behaviour.
4. What happens if granules are over-dried?
Potential effects include brittle granules, increased fines and changes in compressibility. The actual impact depends on formulation and process.
5. Why is LOD important?
LOD provides information about residual moisture. Moisture can influence flow, granule strength, compression behaviour and product stability.
6. What is the relationship between particle size and tablet compression?
Particle size affects flow, packing, die filling and compression behaviour. Significant changes can therefore contribute to weight and tablet-quality variation.
7. What is the difference between CPP and CQA?
CPP relates to a process parameter requiring control because its variability can affect product quality. CQA is a product characteristic that must be controlled to ensure the desired quality.
8. What would you do if LOD fails?
Stop/hold the affected material as required by procedure, document the result, verify the test/sample validity, assess the process parameters and initiate the appropriate investigation and product-impact assessment.
9. How would you investigate excessive fines?
Review raw materials, binder preparation, granulation endpoint, binder addition, drying condition, milling parameters, screen condition, PSD and historical trends.
10. What is the impact of over-lubrication?
It can alter particle surfaces and reduce interparticle bonding, potentially affecting hardness, disintegration and dissolution.
11. How do you ensure representative sampling?
Follow an approved sampling plan based on process and segregation risks, using suitable sampling tools, locations and quantities rather than taking a single convenient sample.
12. What documents should be reviewed before granulation?
The approved BMR/BPR/MFR, applicable SOPs, equipment status, cleaning records, line clearance, material status, calibration status and relevant process instructions.
13. What is the role of IPQA during granulation?
IPQA verifies process/GMP compliance, critical steps, documentation and applicable in-process activities according to site procedures.
14. How can granulation problems lead to compression defects?
Changes in moisture, PSD, density, granule strength or lubrication can change flow, die filling and bonding behaviour, resulting in defects such as weight variation, sticking, capping or lamination.
15. How would you investigate a recurring granulation deviation?
Trend previous occurrences, identify common factors, review equipment/raw-material/process variables, perform structured root-cause analysis, assess systemic causes and implement CAPA or process improvement where justified.
23. Key Takeaways
Effective granulation control is not simply a matter of checking the final LOD or particle size.
The stronger approach is to control the process from the beginning.
- Verify the right material before processing starts.
- Control dispensing and sifting carefully.
- Treat binder preparation as a critical process activity.
- Control dry mixing before liquid addition.
- Monitor granulation parameters and endpoint using the approved process.
- Do not rely only on operator judgement for endpoint determination when validated process indicators are available.
- Control drying based on the established process relationship between parameters and moisture.
- Understand particle-size distribution rather than looking only at average particle size.
- Treat lubrication as a controlled process, not merely a final mixing step.
- Use representative sampling and reliable documentation.
- Investigate abnormalities from a root-cause perspective.
- Always connect CPPs with CQAs and downstream tablet performance.
The most useful mindset for a manufacturing professional is:
Don’t ask only, “Did the batch pass?”
Ask:
“What happened during the process, why did it happen, and do we have evidence that the process remained in a state of control?”
That approach is much closer to effective GMP manufacturing.
WHO describes GMP as a system intended to ensure medicines are consistently produced and controlled according to appropriate quality standards, with written procedures and documented evidence supporting manufacturing operations.
For granulation, this means quality has to be built into the process—not checked only after the granules have already been produced.
24. Regulatory and Technical References
The following sources are appropriate starting points for further reading. They should be interpreted together with applicable national regulations, product-specific requirements and site procedures.
U.S. FDA
FDA’s CGMP framework for finished pharmaceuticals is primarily contained in 21 CFR Parts 210 and 211. Relevant production-control concepts include written procedures, in-process controls, yield calculation, sampling/testing and production record review.
FDA — Current Good Manufacturing Practice (CGMP) Regulations
FDA Process Validation
FDA’s Process Validation: General Principles and Practices provides a lifecycle-based approach to process validation and process understanding.
FDA — Process Validation: General Principles and Practices
ICH Quality Guidelines
ICH Q8(R2), Q9(R1) and Q10 provide an integrated framework around pharmaceutical development, quality risk management and the pharmaceutical quality system.
European Union GMP
EudraLex Volume 4 contains EU GMP guidance, including chapters covering Pharmaceutical Quality System, Personnel, Premises and Equipment, Documentation, Production and Quality Control.
European Commission — EudraLex Volume 4 GMP Guidelines
WHO GMP
WHO provides GMP principles and guidance covering pharmaceutical production, quality assurance and related quality systems. Its GMP compendium provides a broad reference for manufacturers and quality professionals.
WHO — Guidelines: Production and GMP
WHO — Quality Assurance of Pharmaceuticals, Volume 2
PIC/S
PIC/S GMP guidance can be consulted where applicable to the regulatory environment and site quality system.
About the Author
Ramesh Palav is a pharmaceutical manufacturing professional with 21+ years of experience in OSD tablet manufacturing, specializing in Granulation, Compression and Coating, GMP compliance, qualification, validation, QMS and operational excellence.
With hands-on experience supporting USFDA, MHRA, WHO and other regulatory audits, he combines practical shop-floor expertise with a strong focus on process improvement, quality and compliance.
Through Pharma Manufacturing Hub, Ramesh shares practical knowledge, industry insights and career guidance to help pharmaceutical professionals strengthen their technical and GMP capabilities.